Optical Metrology
Precise Measurements with the ZEISS O-INSPECT Multisensor Measuring System (
)
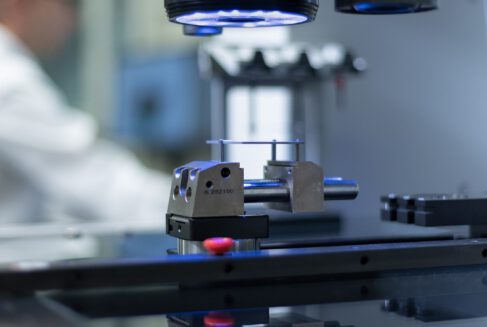
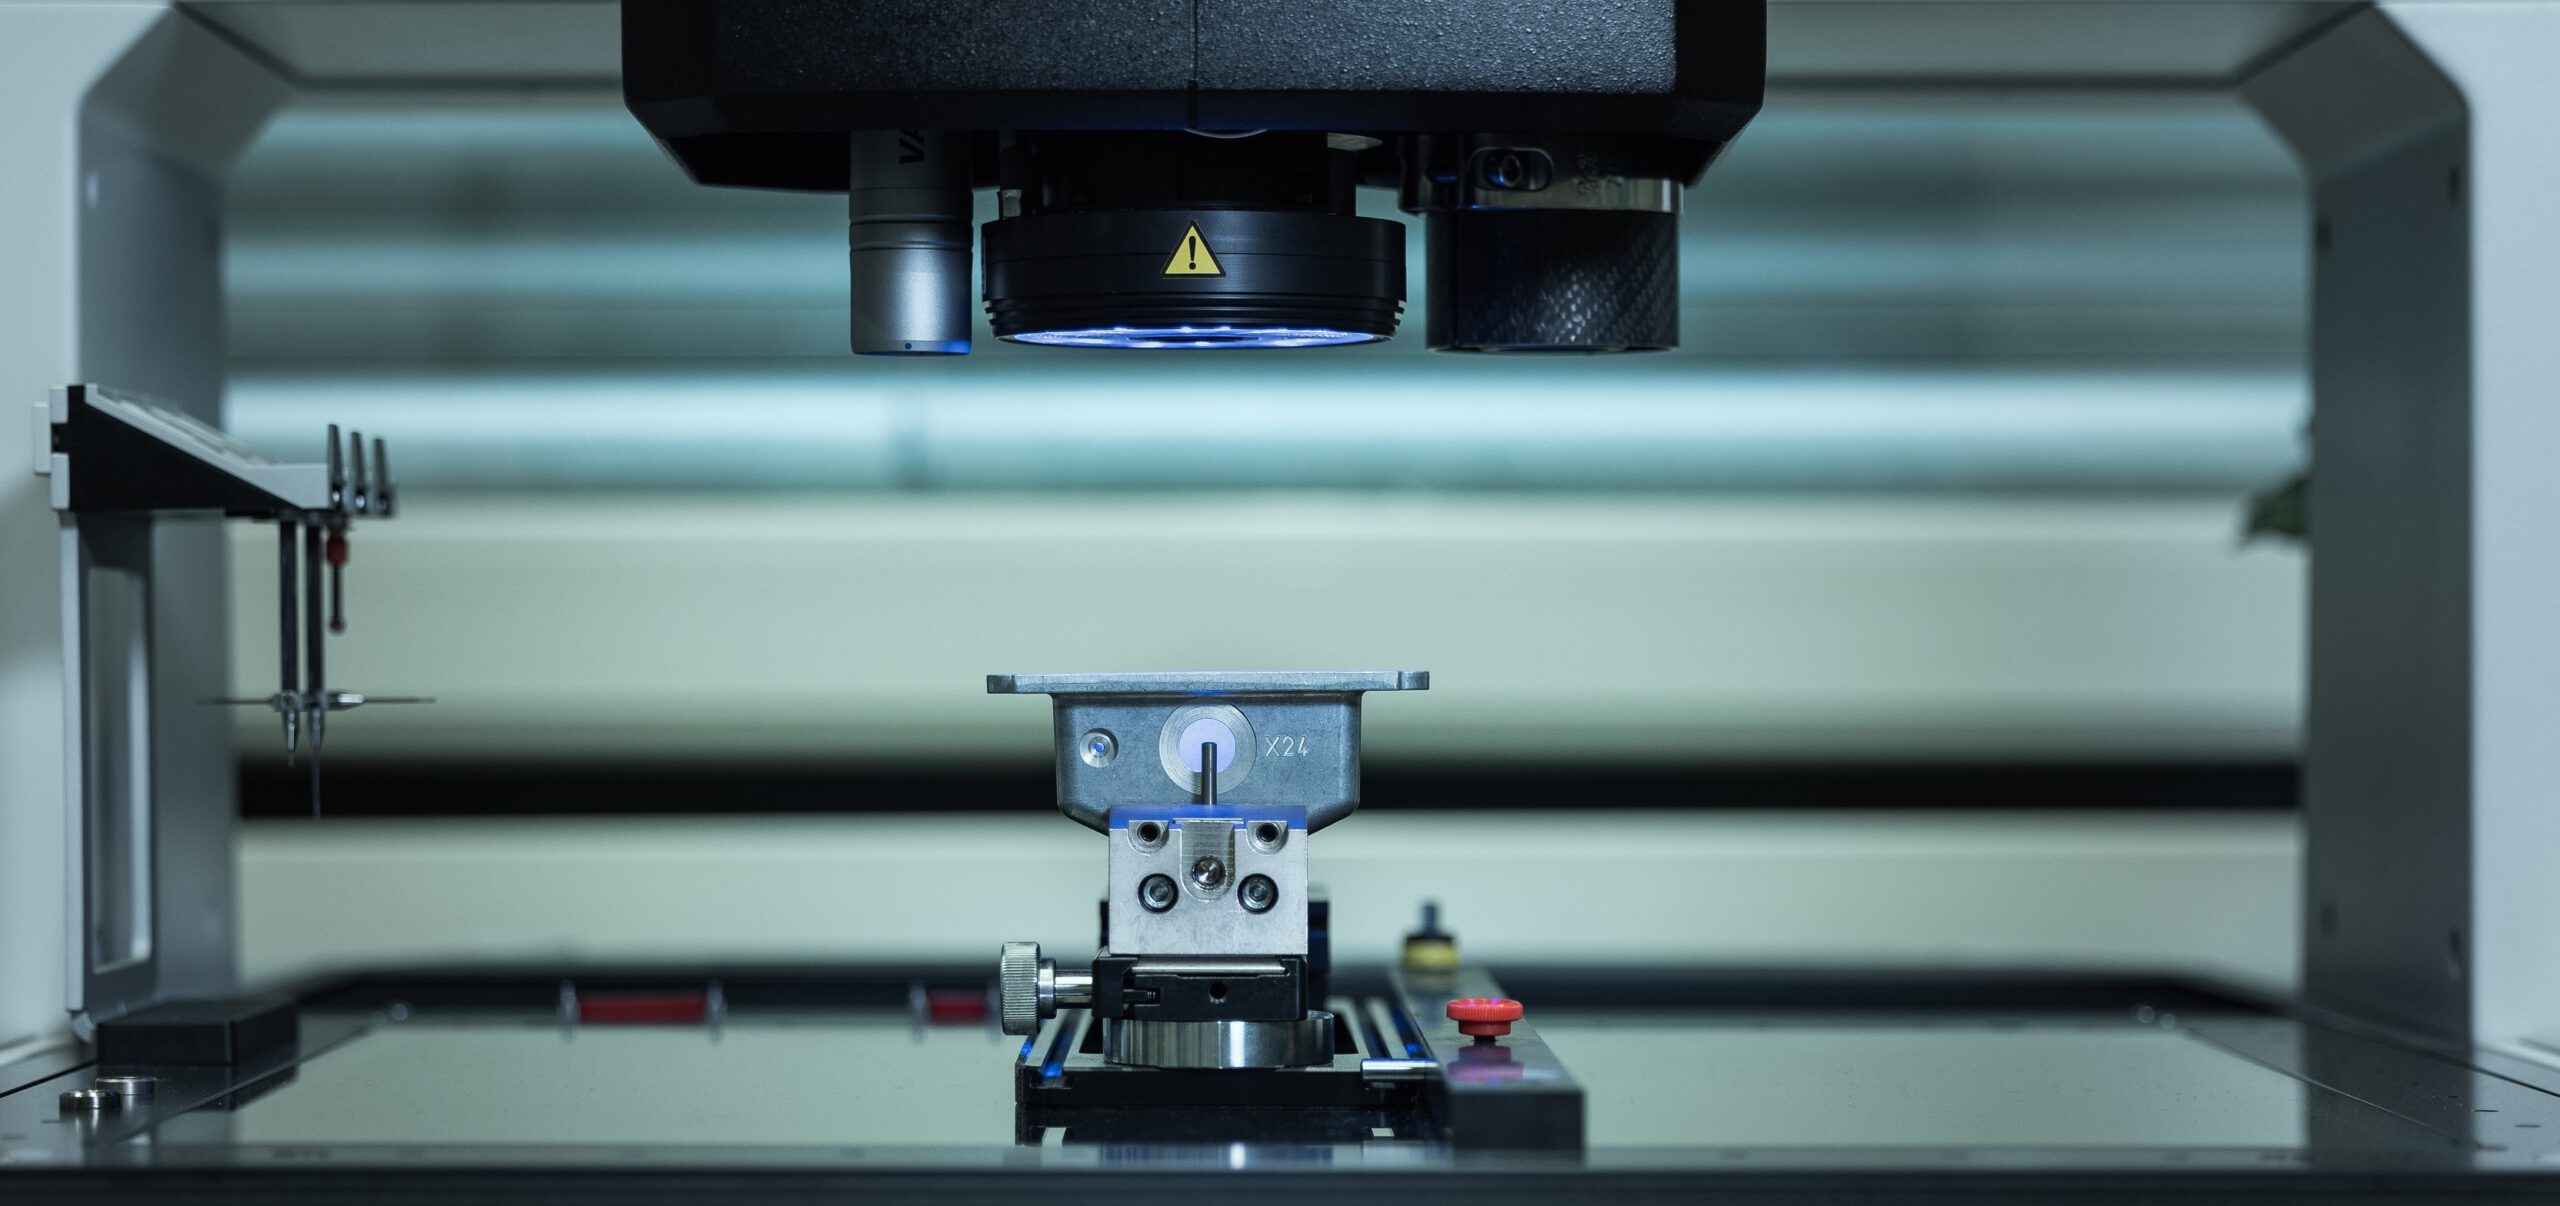
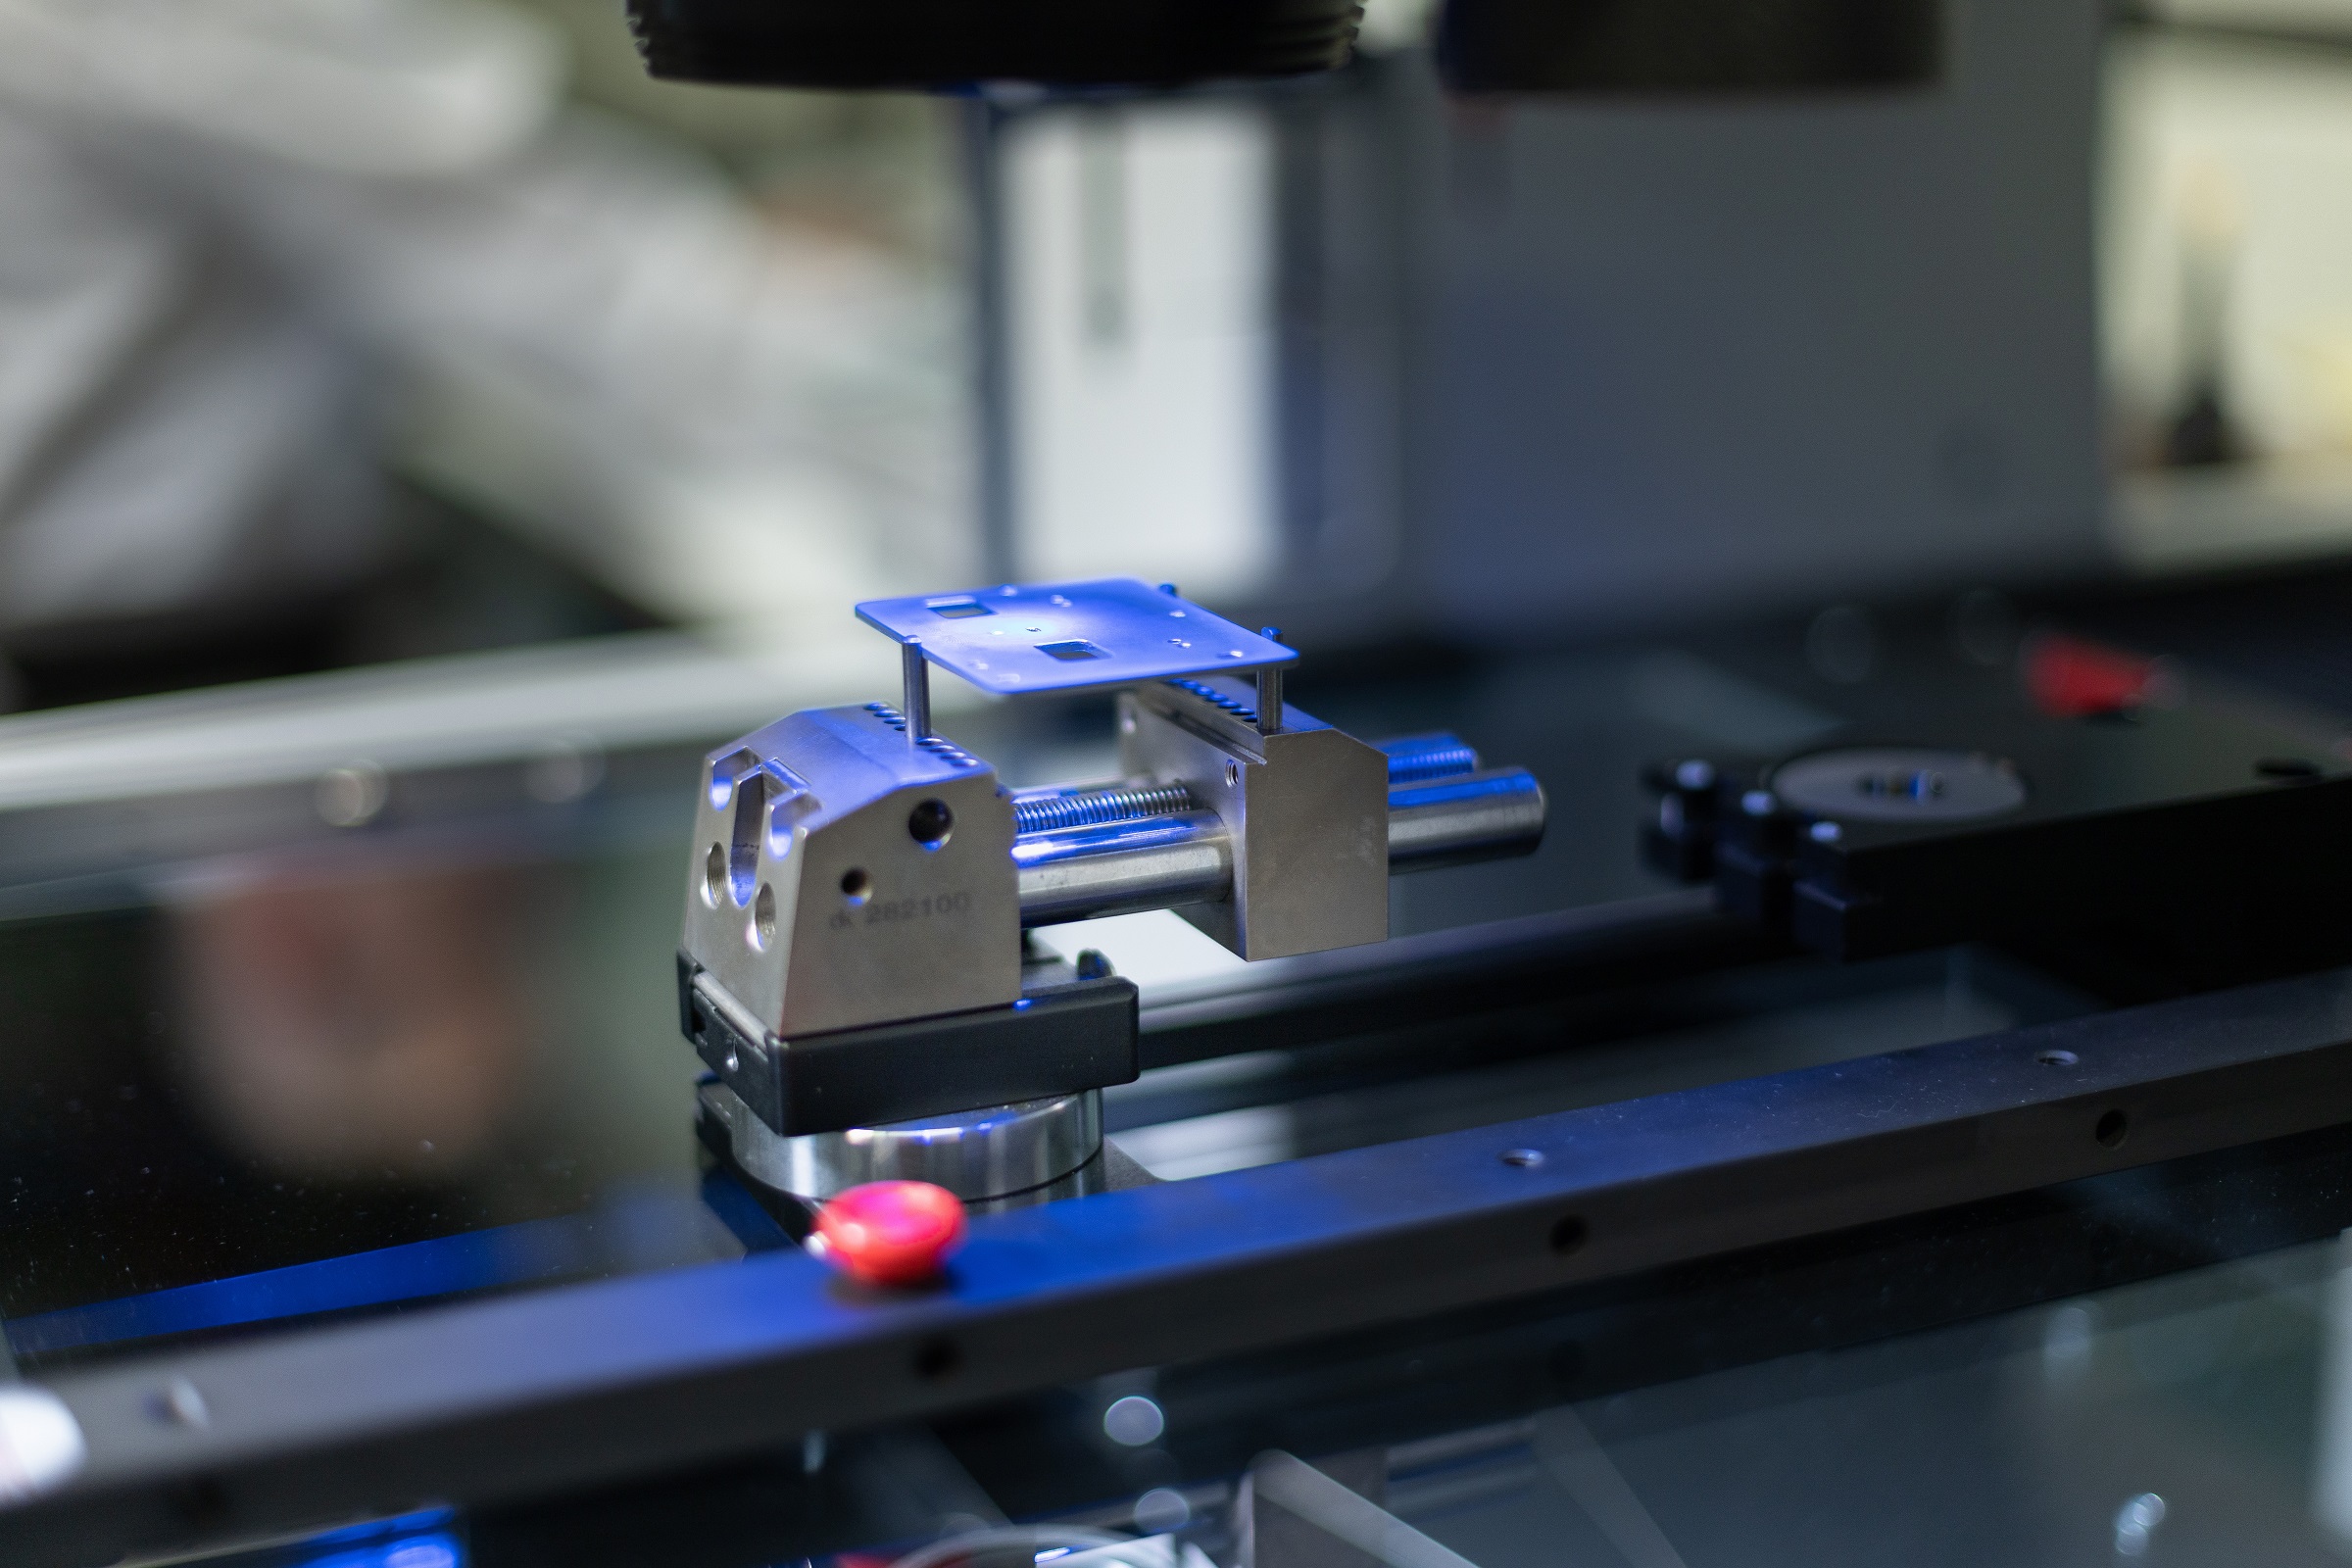
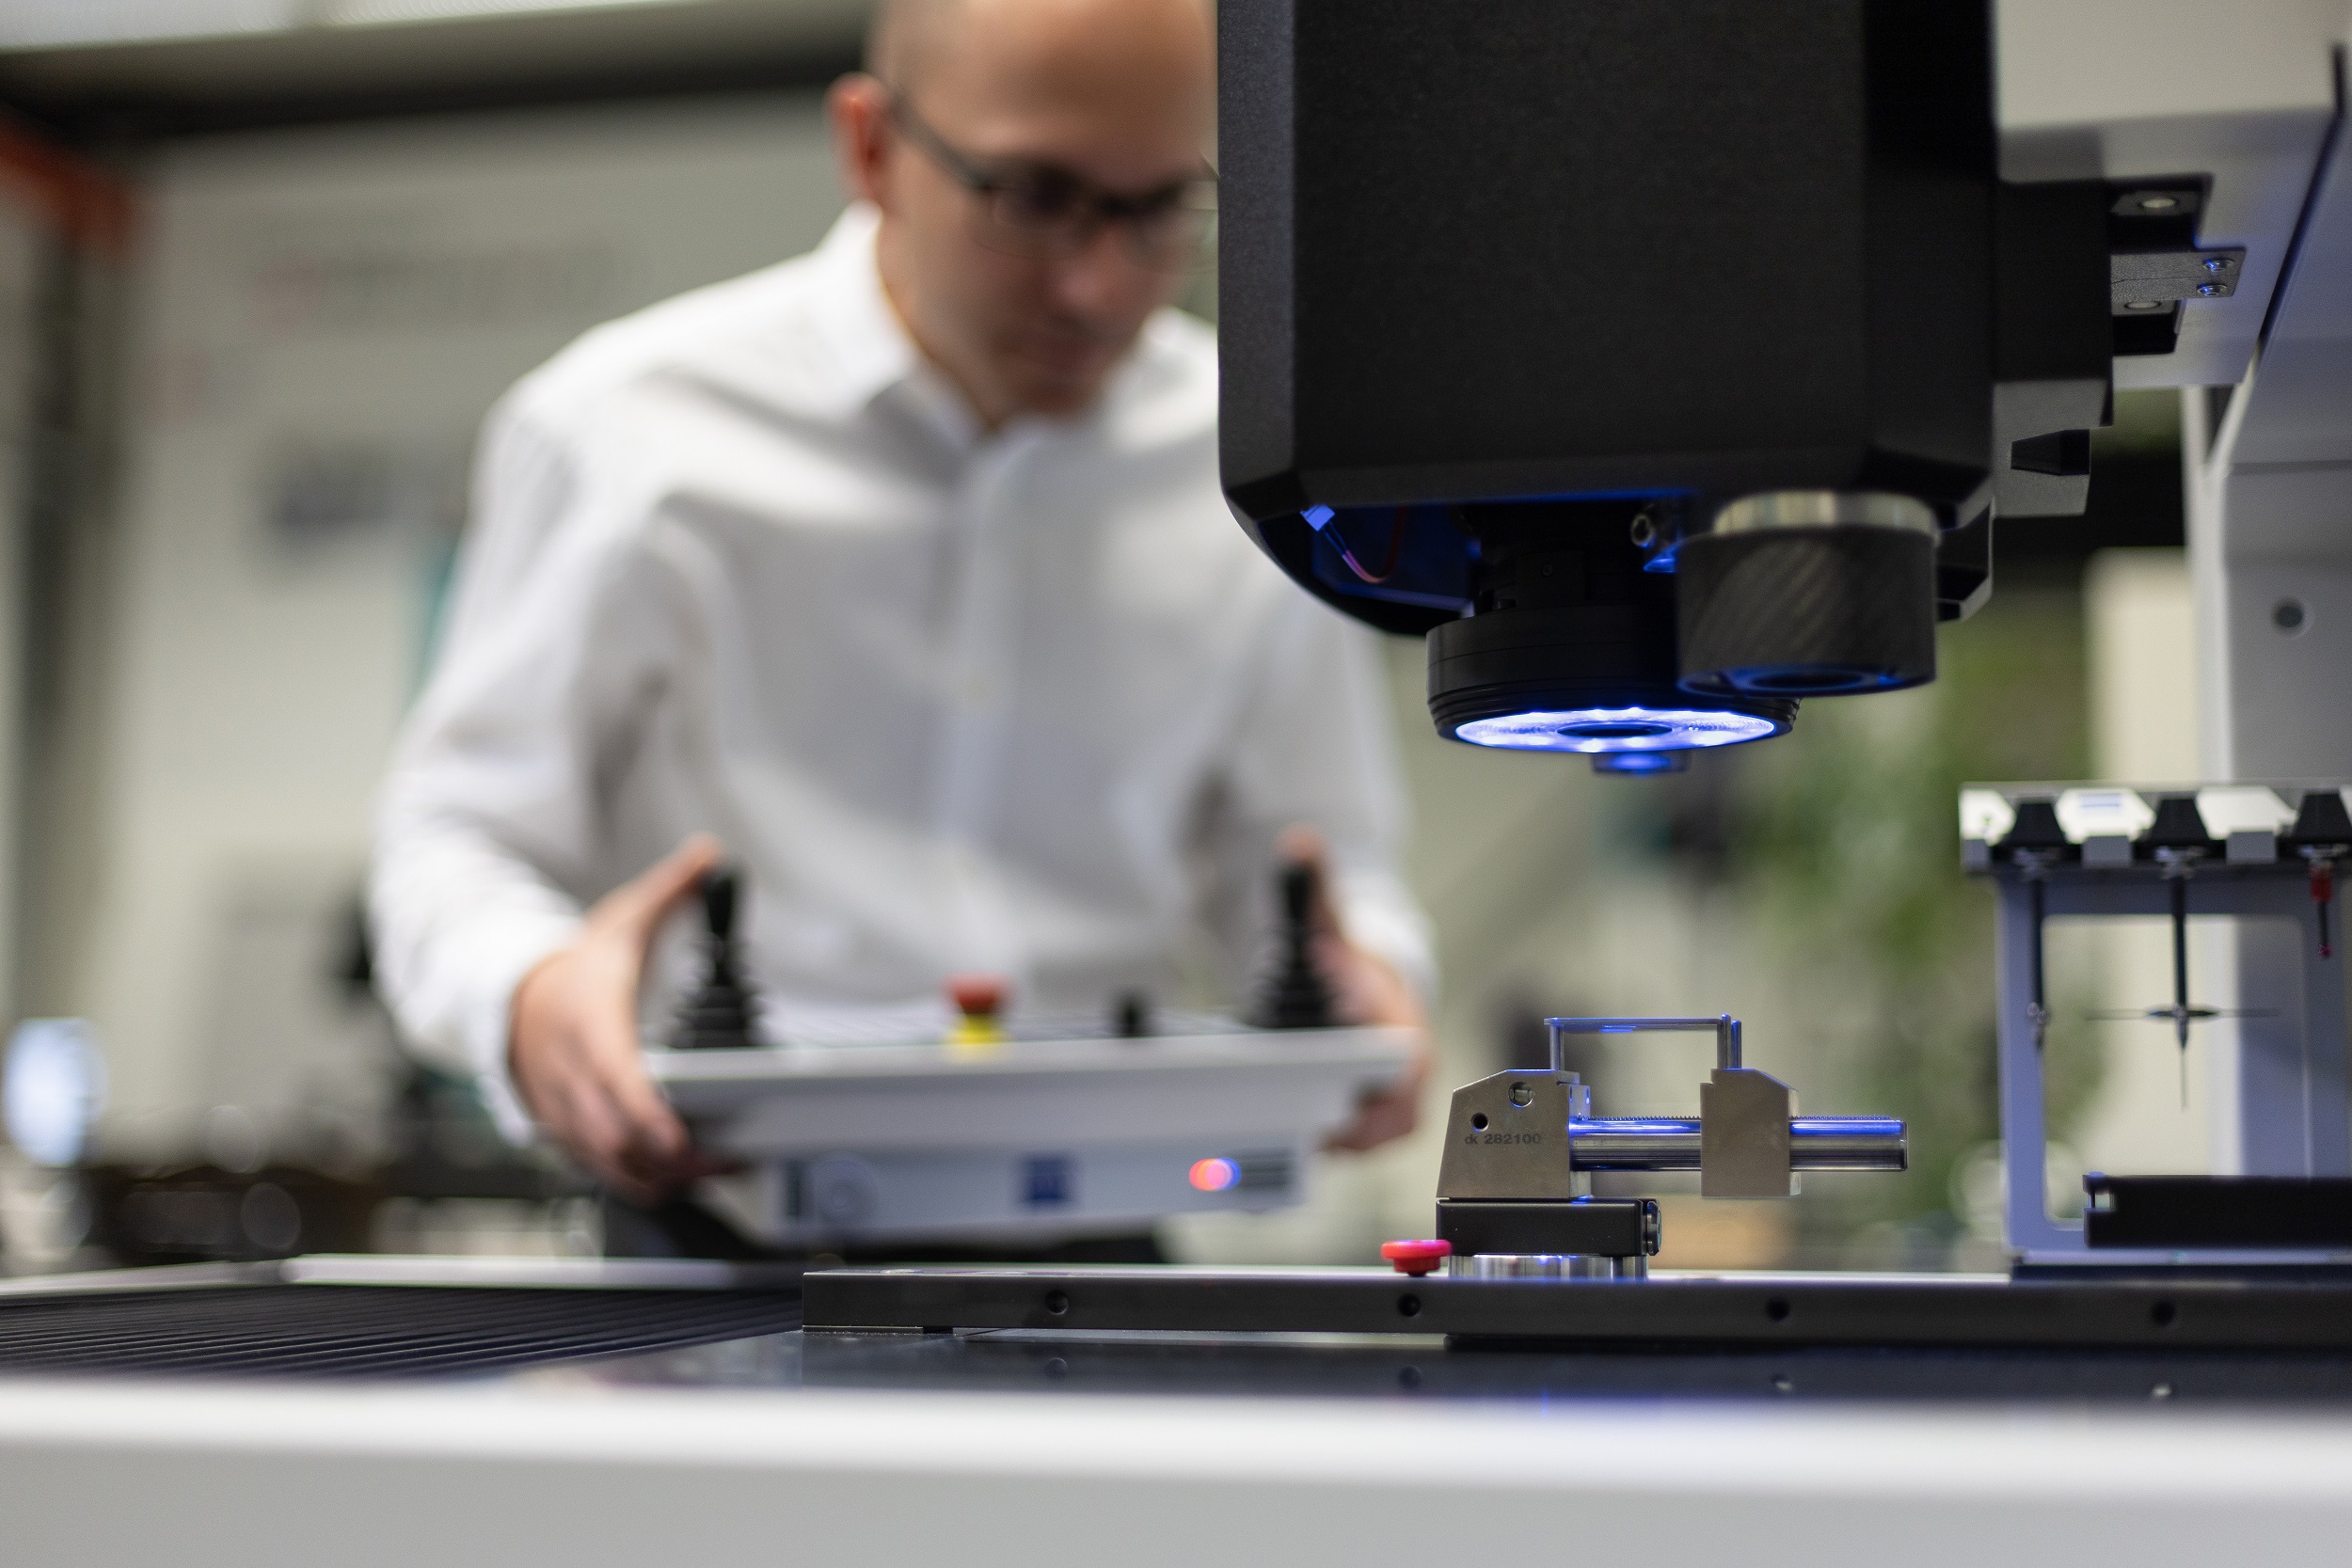
Our optical measurement technology is non-contact and highly precise, thanks to our state-of-the-art multisensor measuring system from ZEISS. This system utilizes various sensors—such as optical sensors, touch sensors, and white-light sensors—to cover a wide range of measurement tasks.
A Wide Range of Measurement Tasks Using Optical Measurement Technology
Optical metrology is a precise method for measuring standard geometries during initial sampling and production inspections. This technology enables fast and accurate measurement of stamped and bent parts, dies, punches, die-cast and injection-molded parts, as well as blanks and printed circuit boards. With the corresponding VDA-compliant test report, the measurement results can be directly evaluated and interpreted, leading to faster and more effective quality control. Contact us and let our experienced 3D measurement technicians advise you.
Using our optical measuring machine combined with a tactile measuring unit (multisensor technology), our specialists perform the following measurement tasks for you:
- Measuring Control Geometry
- Initial sample submissions with a test report in accordance with VDA
- Routine measurements
- Stamped and Bent Parts / Dies / Punches
- Die-cast and injection-molded parts
- Circuit Boards / Printed Circuit Boards
Optical metrology: contactless, fast and full-surface
In optical metrology, the surface of a part is captured without contact. This is ideal for soft, delicate or very small parts that a probe could deform or damage, and for parts with many features that need to be measured quickly. In our lab we use two systems:
- ZEISS O-INSPECT (multisensor): camera, white-light sensor and probe in one machine – optical and tactile features in a single setup.
- GOM ATOS Q (3D fringe projection): captures the entire surface as a dense point cloud – for freeform surfaces, color-coded nominal/actual comparison with the CAD model and 3D digitization.
Optical, tactile or CT?
Optical methods excel with delicate parts, flat parts such as stamped and bent parts or printed circuit boards, and freeform surfaces. For the tightest tolerances on accessible features, tactile measurement is often more accurate; for internal structures, computed tomography. We determine the right method based on part, material and tolerances – often we combine methods. The article CT or tactile measurement? gives an overview.
What you receive
An inspection report with nominal and actual values and an assessment of each feature, on request as an initial sample inspection report according to VDA, and for 3D digitization additionally color-coded nominal/actual comparisons. Turnaround time is usually three to four working days. Optical measurements are outside the scope of our accreditation.
“We’ve got it figured out!”
Frequently asked questions about optical measurement


We’d be happy to advise you!
We would be happy to provide you with personalized advice, with no obligation.
Please contact us.

Learn more about our projects at