Measurement service
Optical Metrology
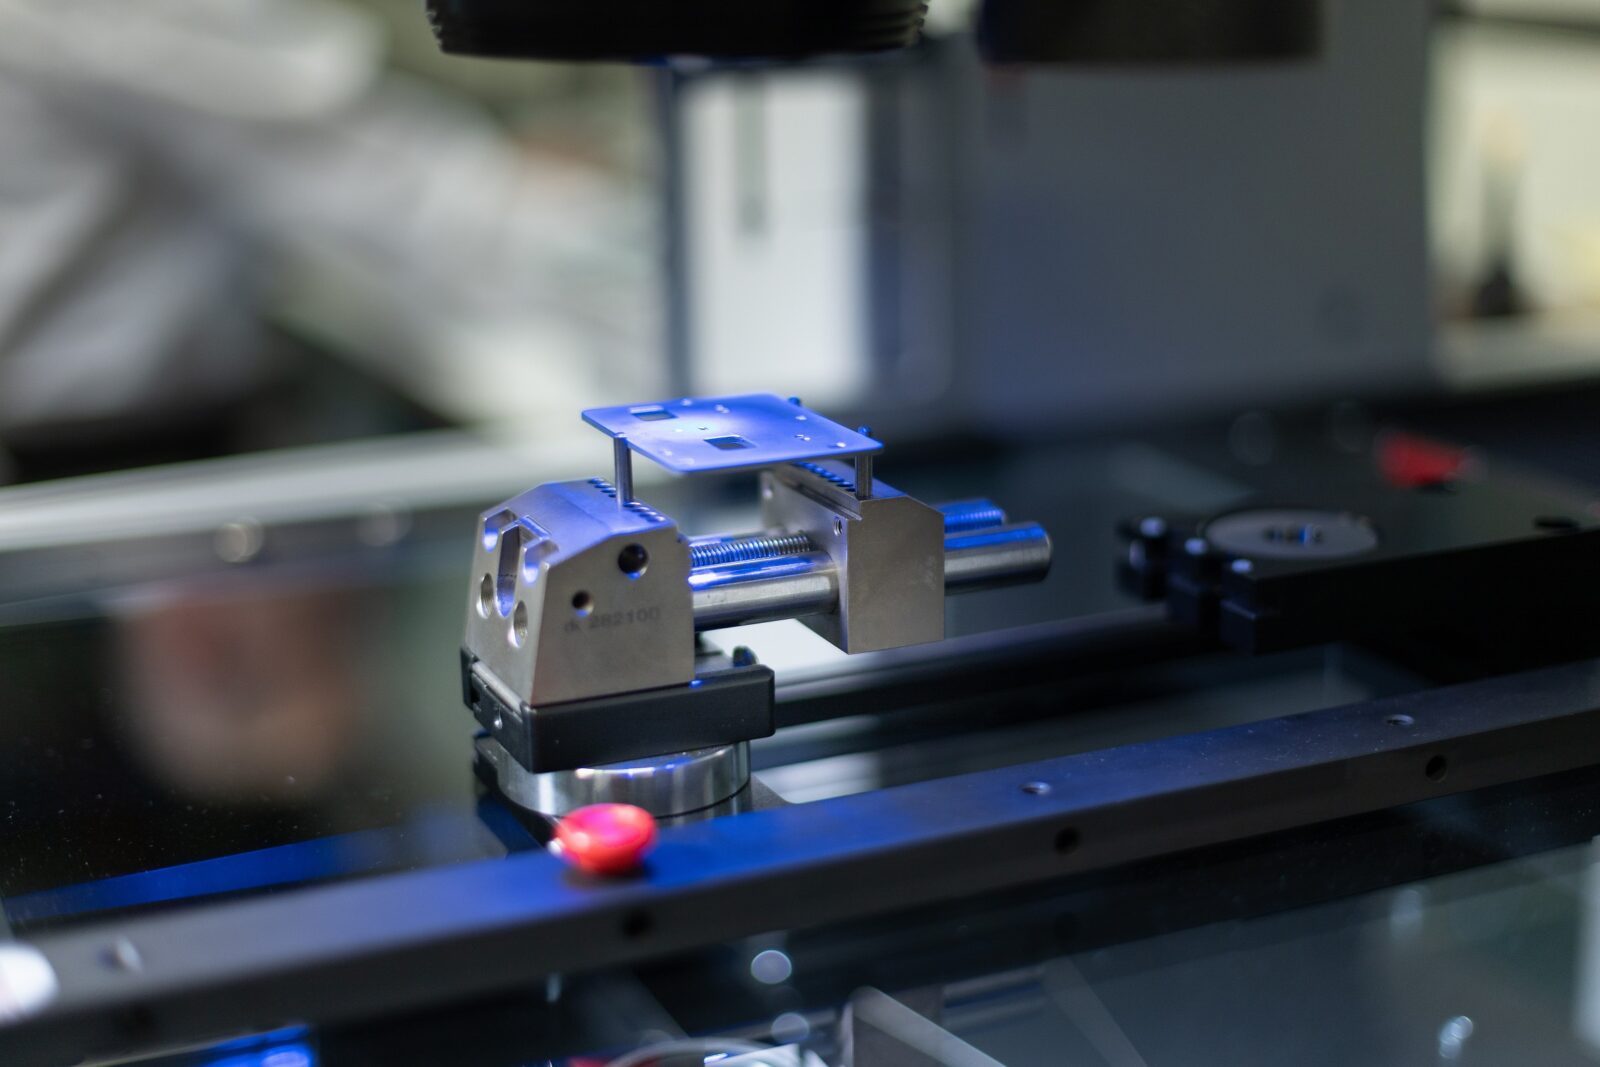
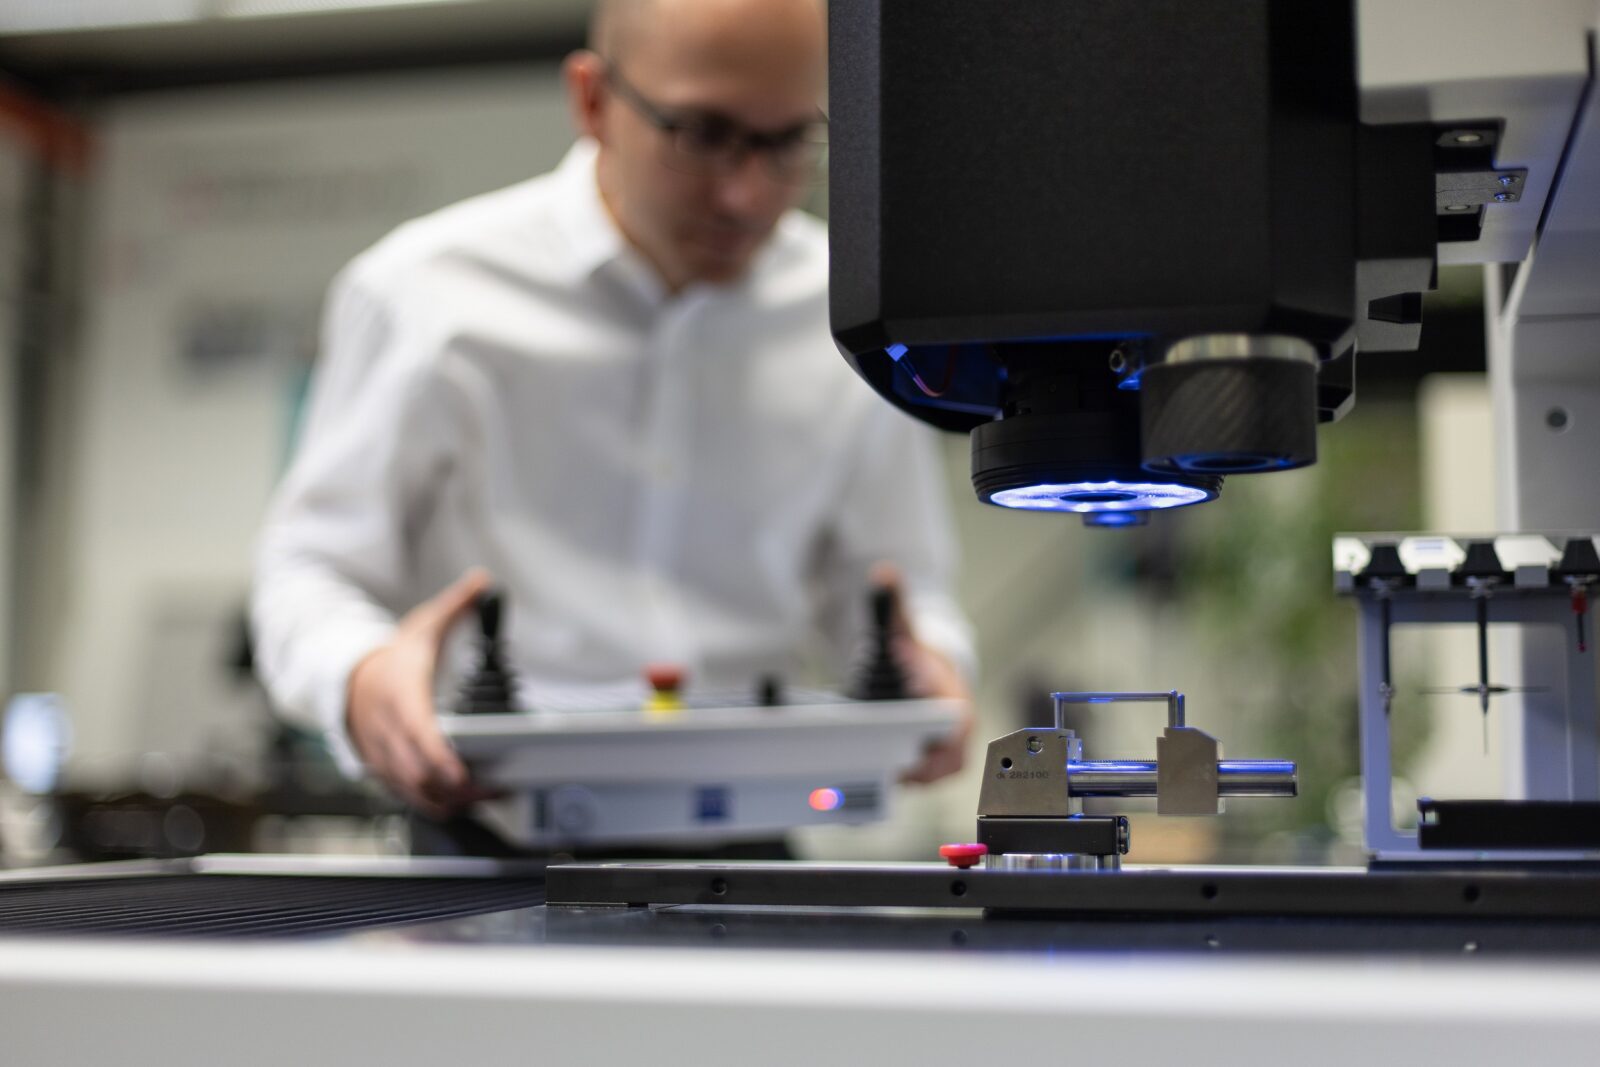
Optical measurement with multisensor technology and fringe projection, mostly contact-free: ideal for delicate, small or flat parts and freeform surfaces. Fast and full-surface, even for parts with many features.
Our systems
Two systems, one goal
ZEISS O-INSPECT (multisensor)
Camera, white-light sensor and probe in one machine: optical and tactile features in a single setup.
GOM ATOS Q (fringe projection)
Captures the entire surface as a dense point cloud: for freeform surfaces, color-coded nominal/actual comparison and 3D digitization.
Measuring principle
How optical metrology works
Optical metrology captures geometry with light instead of a stylus. We use three principles, depending on the feature and the part:
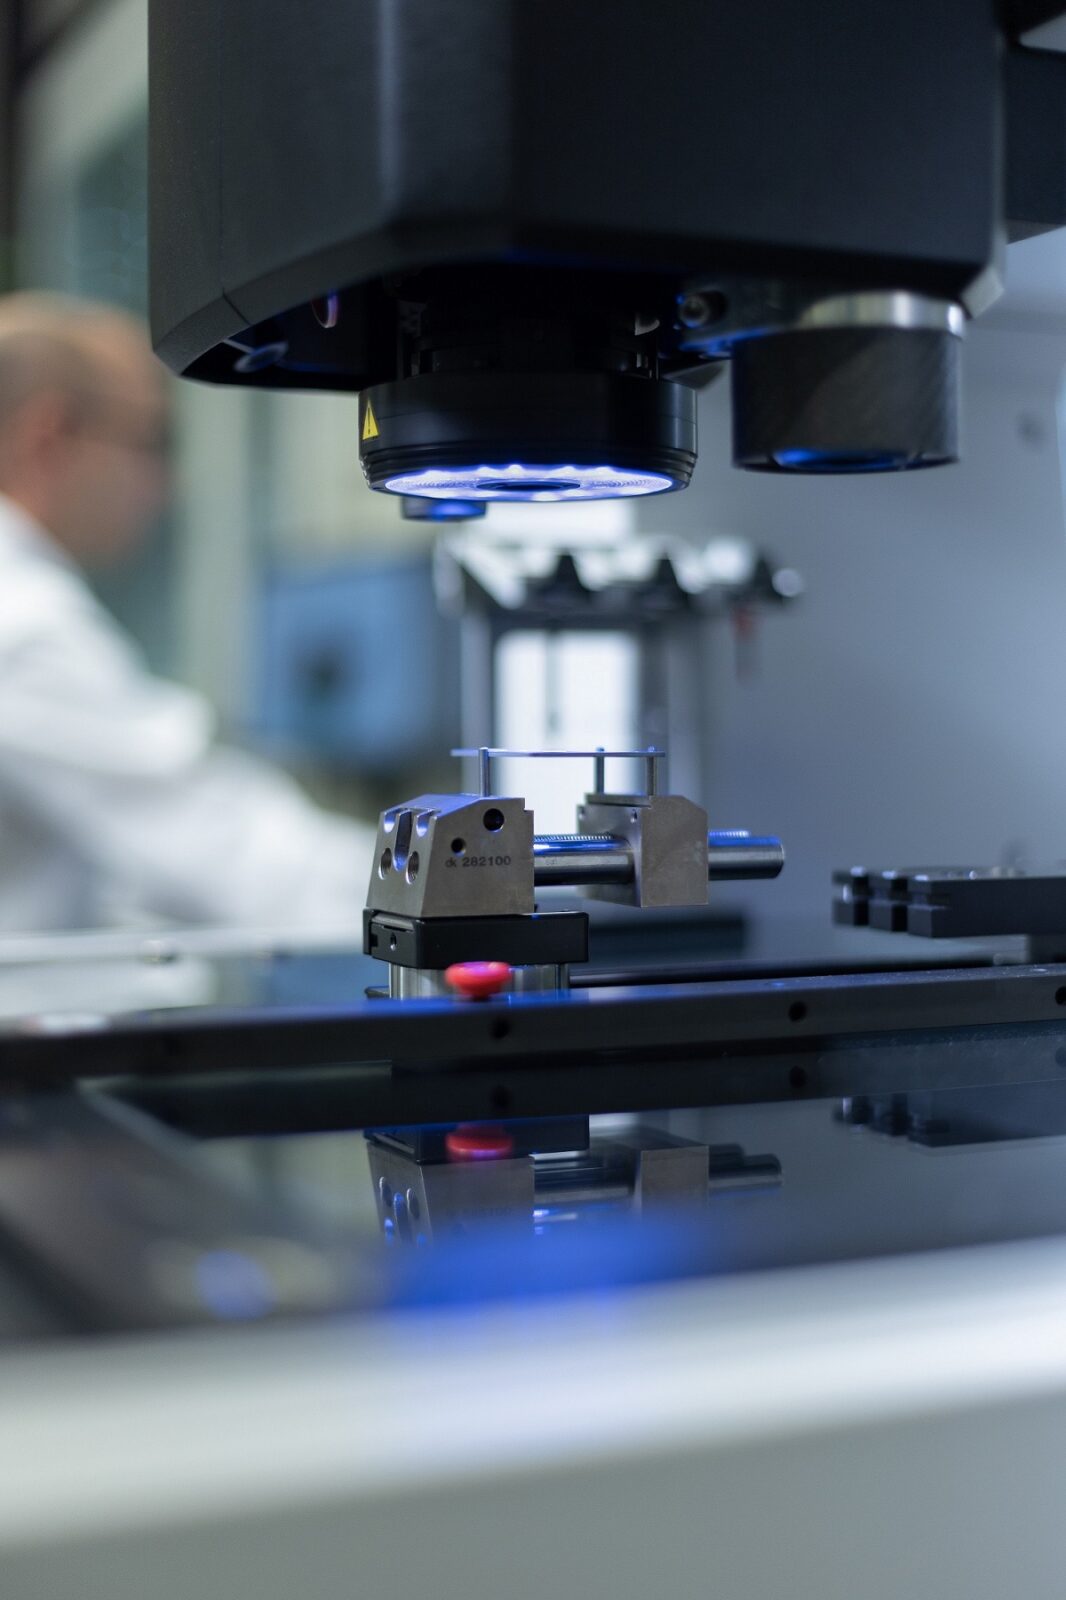
Image processing: A camera detects edges and contours in transmitted or incident light – ideal for flat parts, hole patterns and fine structures.
White-light sensor: Measures heights and flatness point by point without contact, even on soft or delicate surfaces.
Fringe projection: Fringe patterns are projected onto the part; two cameras use them to calculate millions of measuring points across the entire surface.
Measurement tasks
Diverse tasks, solved precisely
Fast and accurate measurement of standard geometries for first article inspections and series measurements, directly with an inspection report according to VDA.
Choosing the method
Optical, tactile or CT?
We determine which method fits based on part, material and tolerances. We often combine methods.
Optical: delicate, flat, freeform
Stamped and bent parts, printed circuit boards, freeform surfaces.
Tactile: tightest tolerances
Often the most accurate on easily accessible features.
CT: internal structures
Whatever cannot be reached from the outside.
Result
What you receive
Optical measurements are outside the scope of our accreditation.
- Inspection report with nominal and actual values and evaluation per characteristic
- On request as an initial sample inspection report according to VDA
- For 3D digitization: color-coded nominal/actual comparisons
Process
Your optical measurement step by step
Send your enquiry
Drawing (PDF), STEP data for the nominal-actual comparison, quantity, and material and surface finish.
Method & quote
We choose O-INSPECT, ATOS Q or a combination with tactile measurement and confirm price and delivery date.
Measurement
Alignment, measurement and evaluation by experienced metrology technicians.
Inspection report
Report with nominal and actual values or a colour deviation map as PDF, usually within 3–4 working days.
FAQ
Frequently asked questions about optical measurement
What is the difference between tactile and optical measurement?
In tactile measurement, a probe captures individual points with high precision. In optical measurement, edges and contours are captured by camera, or the entire surface is captured as a dense point cloud by fringe projection, without contact.
What part sizes can be measured?
From small precision parts to larger assemblies. Highly reflective or transparent surfaces may require pretreatment for optical measurement. It is best to ask us directly.
What data do you need for an optical measurement?
A drawing with tolerances (PDF). For a colour nominal-actual comparison we also need the CAD model, ideally as STEP. Without CAD data we can digitise the part and supply the data, for example as STL.
Is optical measurement accredited?
No. Optical measurements are outside the scope of our ISO/IEC 17025 accreditation. If you need an accredited inspection report, we measure the relevant features tactilely.
What about shiny or transparent parts?
Highly glossy, reflective or transparent surfaces reflect light unfavourably. For fringe projection the surface is therefore pre-treated with a thin matting spray where necessary. Alternatively, we measure such features tactilely or by computed tomography.
How long does an optical measurement take?
The inspection report is usually ready within 3–4 working days of receiving the parts. If your deadline is tight, please contact us directly.
Can optical and tactile features be measured in one order?
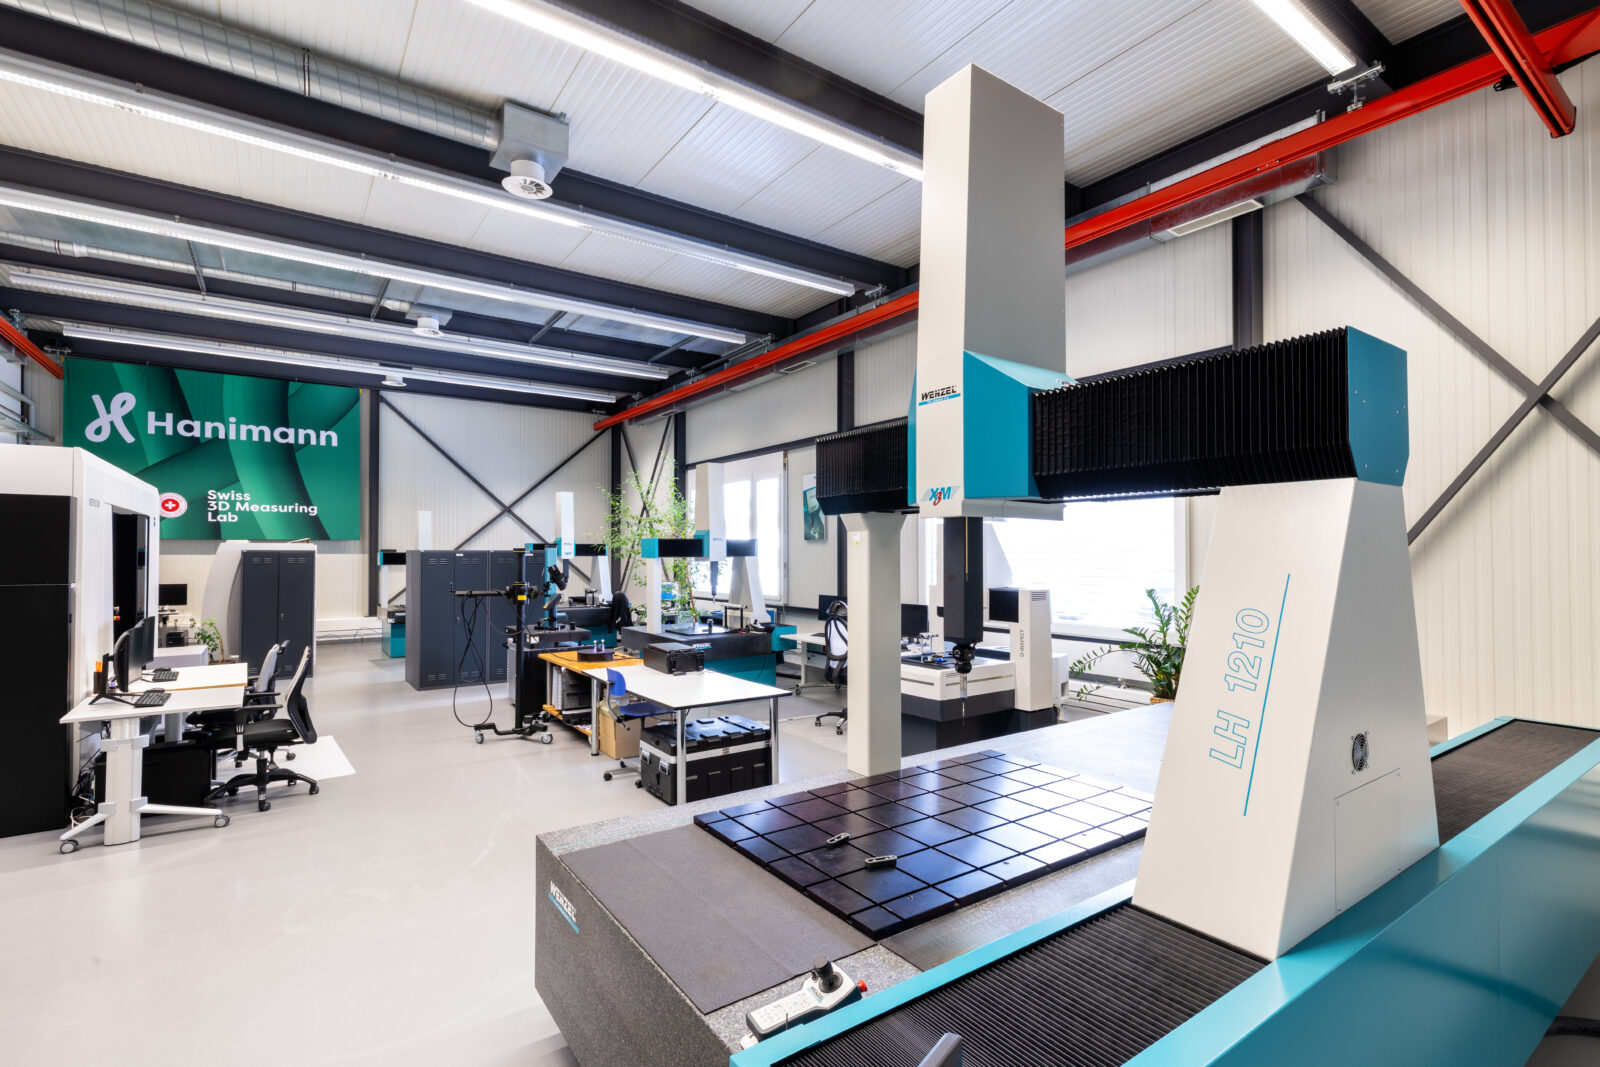
Yes. The ZEISS O-INSPECT combines camera, white-light sensor and probe, so we measure both types of feature in a single set-up. Where needed, we add our coordinate measuring machines or CT.
How much does a measurement cost?
The price depends on part size, complexity, method and batch size. We will be happy to prepare a non-binding quote.
We are happy to advise you!
Get personal, non-binding advice from our experienced 3D metrology technicians.